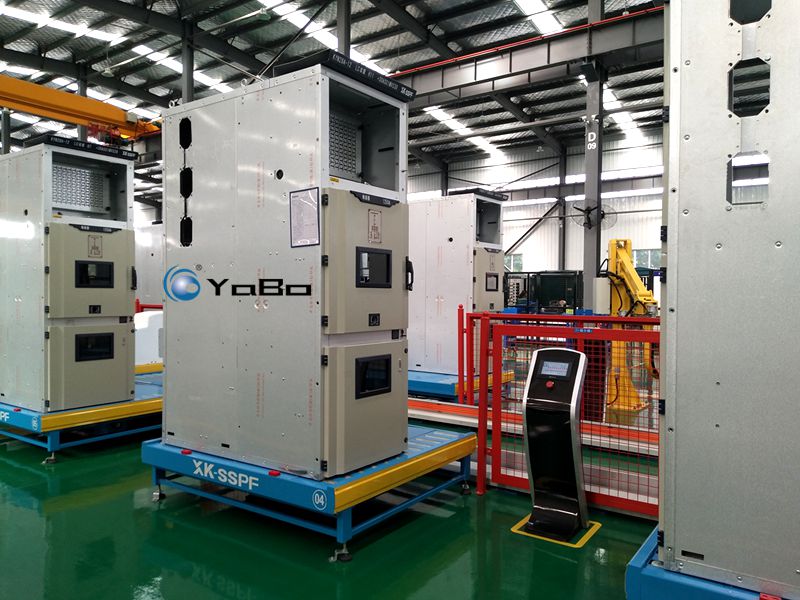

This equipment is an intermittent circulation chain plate assembly line, used for the batch assembly of high-voltage complete electrical equipment. This switchgear assembly line adopts a fixed workstation and workpiece circulation operation mode, suitable for the assembly of 10kV/12kV indoor high-voltage switchgear. It can meet the production needs of medium and high-voltage cabinets with different specifications and configurations, as well as generalized, modular, and customized production requirements. The entire switchgear production line is centered on process standardization and heavy-duty stable operation, adapted for large-scale mass production scenarios.
1. Adaptable Assembly Product Range
The production line primarily adapts to the KYN28-12 armored removable AC metal-enclosed switchgear (central cabinet), while also compatible with mainstream high-voltage cabinet types of the same voltage level and structural weight. It supports flexible production of multiple categories, and adaptable specifications can be customized.
- Core Adaptable Cabinet Type: KYN28-12 series 10kV central cabinets, with cabinet width specifications of 650mm, 800mm, 1000mm, and 1200mm, including ordinary types, reinforced insulation types, high-current types, and other subcategories.
- Compatible Expansion Cabinet Types: Adaptable to XGN15, XGN24, and other fixed metal-enclosed switchgear, small ring main unit (RMU) enclosures, and related cabinet assembly; suitable for 12kV and 24kV medium-voltage cabinet production.
- Cabinet Parameter Adaptation (Customizable): Adaptable to cabinet shell weights of 800kg–1500kg, with a maximum finished product load capacity of ≤2 tons; supports differentiated customization of cabinet dimensions, mounting hole positions, and compartment structures. Assembly workstations and tooling positioning structures can be adjusted according to product processes.
- Electrical Parameter Adaptation: Adaptable to cabinet assembly with rated currents of 630A–4000A, power frequency withstand voltage of 42kV, and lightning impulse withstand voltage of 75kV, meeting production standards for distribution, industrial and mining, new energy, and substations.
The above cabinet types all adopt a four-compartment structure (circuit breaker compartment, busbar compartment, cable compartment, instrument compartment). The production line can adapt to cabinet assembly with different compartment layouts and component configurations, compatible with the entire process of empty shell pre-assembly, semi-assembly, and complete machine commissioning.
2. Production Line Equipment Architecture
The entire line adopts a closed-loop circulation chain plate conveying structure, with fixed workstation operation and dynamic workpiece circulation as the core. It integrates mechanical conveying, electrical control, safety protection, and auxiliary lifting, realizing intermittent conveying, workstation positioning and locking, and process interlocking. The overall structure is modular and can be customized according to needs for line length, number of workstations, and load rating. This type of switchgear assembly line usually consists of four parts: the conveying system, control system, protection system, and lifting system, each of which can be configured independently.
2.1 Main Line Conveying Mechanical System
The conveying main body adopts a combination of aluminum alloy and heavy-duty steel structure guide rails, with dual-chain synchronous drive. It has strong load-bearing capacity, low operating noise, and is wear-resistant and durable, suitable for continuous operation of heavy cabinets. The line body adopts intermittent conveying; workpieces automatically stop and lock in position upon reaching the workstation, and circulation is triggered after the process is completed, with no idle running.
The line body has a built-in double-layer track: the upper layer is the workpiece operation conveying track, and the bottom layer is the tooling plate return track. Lift-and-transfer mechanisms are configured at both ends to realize automatic closed-loop circulation of tooling pallets, eliminating the need for manual handling and return.
Supporting heavy-duty tooling pallets are made of welded steel plates, equipped with anti-collision structures and workstation number identification. The bottom of the pallet is equipped with positioning mechanisms and blocking trigger sensing components to ensure no deviation when stopping at the workstation. The tabletop reserves anti-slip limit adjustment structures, which can adjust the positioning distance according to cabinet specifications, adapting to multi-size cabinet fixation, and avoiding displacement, collision, and tipping during lifting and assembly.
The entire line drive unit adopts a heavy-duty motor reducer configuration, with a single workstation rated load of ≥2 tons, meeting the conveying needs of shells and finished products. The start and stop buffering is controllable, protecting the cabinet sheet metal and internal structure.
2.2 Electrical Control System
The entire line adopts a PLC distributed control system with industrial bus signal transmission, realizing equipment linkage, signal acquisition, fault self-diagnosis, and process interlocking. It supports parameter debugging and program upgrades, adaptable to different production rhythms and process requirements.
The equipment is configured with a vertical operation console, integrating a touch screen, start/stop buttons, workstation call buttons, and emergency stop buttons. It features entire line start/stop control, workstation status monitoring, operation data statistics, fault alarm prompts, and manual fixed-point positioning functions, supporting both manual and automatic control modes.
Each assembly workstation reserves industrial power supply interfaces and pneumatic quick-plug interfaces, which can directly support electric wrenches, pneumatic tools, and testing instruments without the need for external long cables or air pipes. The number and layout of interfaces can be adjusted according to workstation process requirements.
2.3 Safety Protection System
The entire line is equipped with metal mesh safety isolation fences, physically isolating the movement area from the personnel operation area to prevent accidental entry. The fence reserves dedicated maintenance safety doors equipped with safety interlock switches; opening the door triggers an entire line stop.
A global emergency stop interlock loop is set up, integrating operation console emergency stop, workstation emergency stop, and fence maintenance door safety signals. If any condition is triggered, the entire line stops immediately. The entire line is equipped with overload protection, short-circuit protection, limit protection, and anti-jamming protection functions.
2.4 Auxiliary Lifting Equipment System
The production line is equipped with two types of lifting equipment to adapt to loading/unloading and heavy component assembly:
- Column-mounted Jib Crane (with electric hoist): Installed on the side of the workstation for local precise lifting at a single workstation, meeting the assembly needs of empty cabinet loading, circuit breaker trucks, copper bars, insulators, and other heavy accessories.
- Overhead Bridge Crane (factory roof): Responsible for bulk cabinet blank loading, finished product offline, and cross-workstation transfer of large items, adapting to mass production rhythms.
The tonnage and operating radius of the lifting equipment can be matched according to production needs.
3. Assembly Process Flow (Workstations can be added or reduced as needed)
The entire line process conforms to the high-voltage switchgear assembly process, adopting the mode of workpiece circulation and fixed workstations. Workstations can be increased or decreased according to production capacity and process standards. The standard process is as follows:
- Loading Workstation: Hoist the empty cabinet shell onto the tooling pallet, complete positioning and locking, and input production information.
- Cabinet Pre-treatment Workstation: Complete cabinet shaping and sheet metal calibration; install internal compartment partitions, fixed brackets, grounding systems, and complete cabinet fasteners.
- Primary Main Circuit Assembly Workstation: Install insulators in the busbar and cable compartments; complete bending, assembly, docking, and fastening of main circuit copper/aluminum bars.
- Truck Compartment Assembly Workstation: Install circuit breaker truck guide rails, limit mechanisms, propulsion mechanisms, and mechanical interlocks; debug the basic stroke of truck propulsion and extraction.
- Instrument Compartment Assembly Workstation: Assemble instrument door panels and observation windows; fix secondary components such as relays, changeover switches, control devices, and indicator lights.
- Secondary Wiring Workstation: Complete secondary control wire routing, terminal crimping, circuit wiring, and wire number identification.
- Mechanical Debugging Workstation: Debug cabinet door opening/closing interlocks, truck mechanical actions, and five-prevention interlock mechanisms; verify the accuracy and reliability of mechanical actions.
- Energization and Withstand Voltage Test Workstation: Conduct circuit energization tests, insulation tests, power frequency withstand voltage tests, and simulated working condition tests to eliminate electrical hazards.
- Finished Product Offline Workstation: Qualified finished switchgear is hoisted offline and put into storage; empty tooling pallets are automatically returned to the loading workstation via the lift-and-transfer mechanism, entering the next production cycle.
The entire switchgear production line uses fixed cycle times and automatic circulation to ensure continuous process connection, reducing work-in-progress accumulation and transfer losses.
4. Core Advantages and Customization Capabilities
4.1 Improvements over Traditional Assembly Modes
Traditional assembly uses cabinet floor placement and manual trolley transfer, leading to problems such as cabinet collision and deformation, chaotic workstations, non-standard processes, poor quality consistency, high labor costs, and low site utilization. This assembly line adopts pipeline operation, with workers at fixed workstations and automatic workpiece circulation. The process division is clear, and the operation standards are unified, reducing handling frequency and lowering collision and assembly deviations. The closed-loop circulation structure eliminates the need for manual tooling transfer, improving production rhythm and site utilization, suitable for large-scale, standardized mass production.
4.2 Customizable Parameters and Configurations
- Line Body Parameters: The total length, width, and height of the line body can be customized according to the workshop site. 8–16 standard workstations can be set, adaptable to single-line, double-line, and circular layouts.
- Load Parameters: Standard load is 2 tons; heavy-duty versions can be upgraded to adapt to heavy cabinets of 3 tons and above. Different sizes of tooling pallets can be customized to adapt to non-standard cabinets.
- Process Configuration: Modules such as coding, automatic fastening, testing, and data traceability can be added. Workstation sequence can be adjusted, and special process workstations can be added or reduced according to process standards.
- Control Functions: Supports production data statistics, capacity monitoring, and fault traceability. Can be connected to MES systems. Manual/automatic/semi-automatic operation modes can be customized.
- Protection Configuration: Dust-proof and noise-reduction configurations can be customized according to different workshop environments. Fence styles, emergency stop layouts, and interlock logic can be customized.
5. Core Equipment List Summary
| Equipment Name | Model/Structural Features | Core Purpose |
|---|---|---|
| Assembly Base | 12kV central cabinet/fixed switchgear, multi-spec customizable | Core assembly workpiece of the production line |
| Chain Plate Circulation Assembly Line Body | Steel structure + aluminum alloy guide rail, dual-chain drive, closed-loop circulation | Automatic circulation conveying of tooling pallets and cabinets |
| Heavy-duty Tooling Pallet | Steel plate welding, with positioning lock, anti-collision structure, workstation number ID | Load and fix cabinets, adapt to multiple specifications |
| Vertical Operation Console | Touch screen + function buttons + emergency stop, PLC control | Entire line control, status monitoring, fault alarm, parameter setting |
| Safety Isolation Fence | Metal mesh frame, with interlock maintenance door | Safety isolation, interlock stop protection |
| Blocking, Lift-and-transfer Mechanism | Line body integrated, automatic sensing start/stop | Workstation positioning, pallet direction change and return, closed-loop circulation |
| Column-mounted Jib Crane | Rotating boom + electric hoist | Lifting of cabinets and heavy parts within the workstation |
| Overhead Bridge Crane | Factory roof mounted, large span | Batch loading, finished product offline, cross-area transfer |
| PLC Electric Control System | Industrial bus modular control, full process interlock | Logic control, signal acquisition, linkage, safety protection |